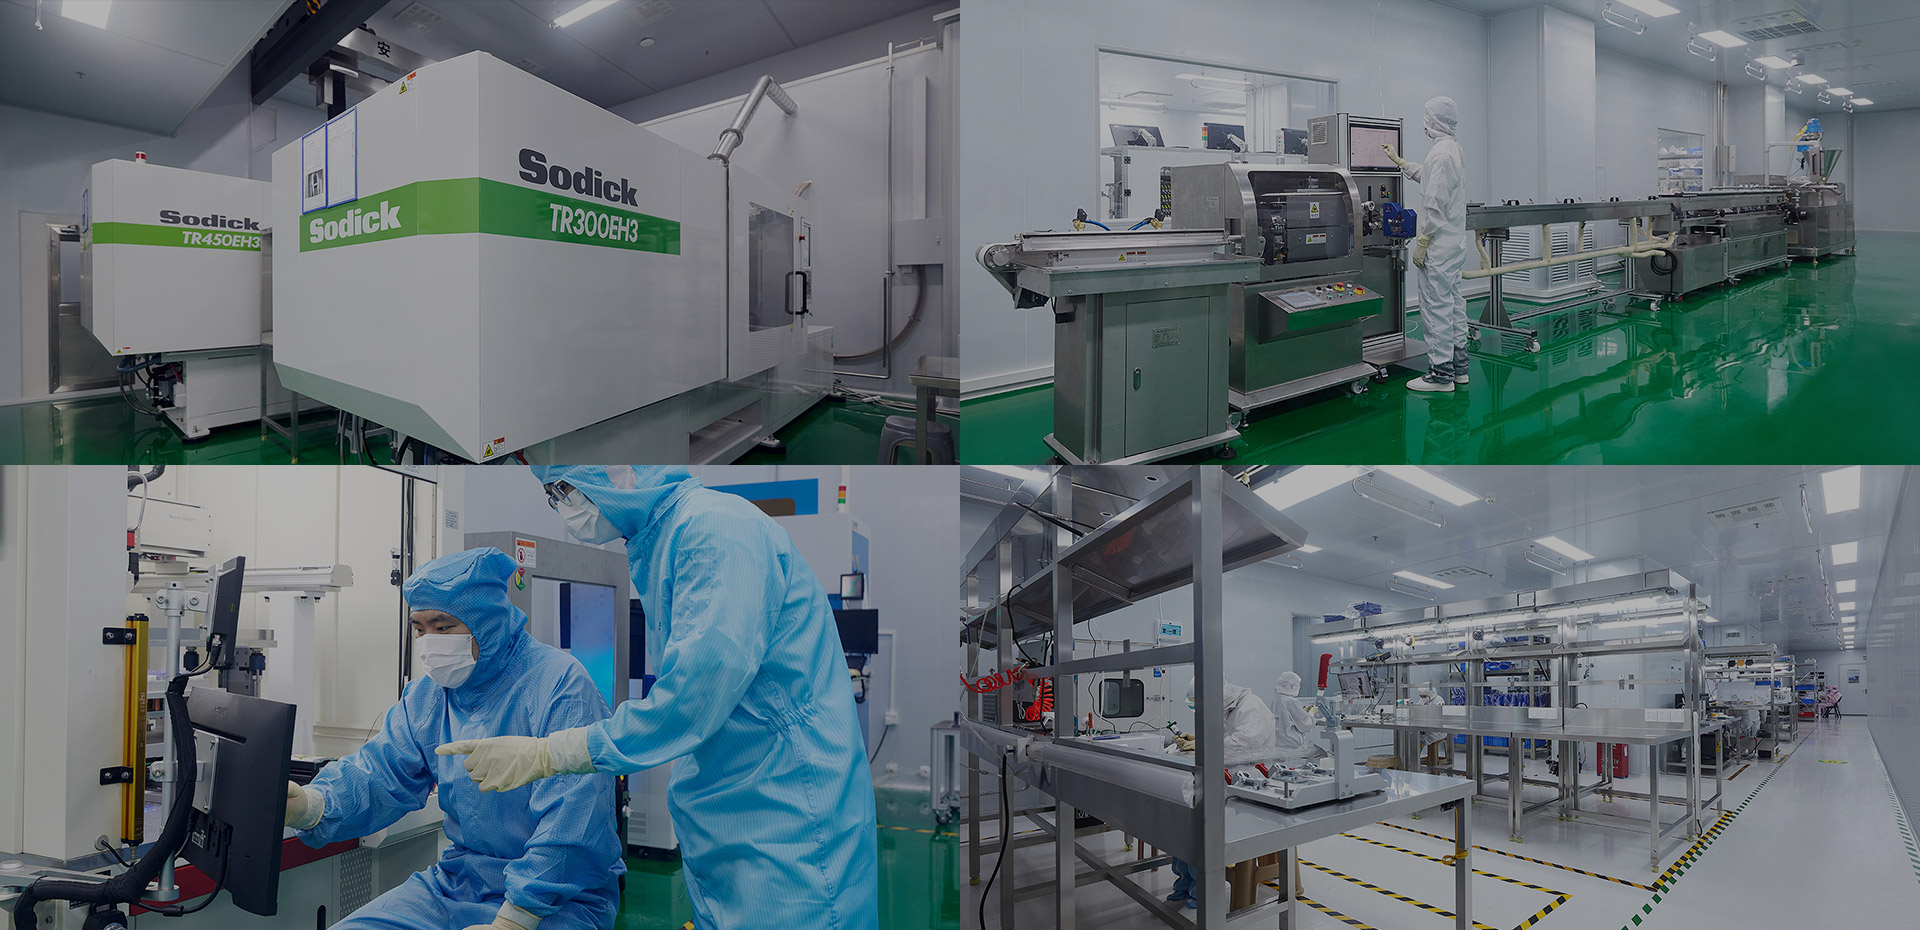
Where it breaks — and why you notice it late
Quality problems don’t announce themselves politely; they show up as line stoppages, customer returns, and ugly audit findings. If your medical device assembly line is a bottleneck for product release, you’re seeing symptoms: inconsistent incoming parts, shifting fixturing tolerances, or batches that pass final inspection but fail performance. I want you to treat those symptoms as signals you can act on, not inexplicable chaos. Start by mapping what comes in, then map what happens to it on the line.
Experience that matters and one big industry signpost
I’ve worked alongside med-tech engineers and QC leads to design IQC gates and in-process checks that actually prevent escapes — not just catch them. Practical controls like disposition rules, matched-material lot tracking, and fixture validation matter. Industry conversation at MD&M West regularly highlights problems and fixes around laser joining methods, which mirrors what we see on the floor: tighter weld control reduces rework. The same trade discussions that surface there also point to advances in medical device laser welding, and those advances are documented across standards and conference papers. Trust the combination of field-tested routines and published best practices when you choose process controls.
Common failure modes and direct fixes
Stop chasing vague root causes. If incoming parts vary, require certificate-of-conformance plus a fast incoming check that verifies critical dimensions and surface finish before parts hit assembly. If in-process drift shows up, lock down fixture repeatability with gage R&R and a daily validation shim. For joining defects — porosity, cold welds, misalignment — enforce immediate rollback to a validated setup and capture a process signature (power/time/force). Use quick SPC charts for key characteristics and trigger immediate containment rather than batch-level inspection after the fact.
Choosing between IQC-first and IPQC-first approaches
IQC-first makes sense when you have high supplier variability: stop bad parts from contaminating your process. IPQC-first works when suppliers are stable but your assembly introduces variability. Don’t pick a side forever. The pragmatic move is a staged approach: start with tight IQC on new suppliers or new part numbers, then normalize to lighter IQC with robust IPQC checkpoints once supplier performance proves stable. Automation helps, but only after you’ve locked process windows; sensors and inline vision are powerful, but they duplicate poor process discipline if your fixtures and supplier controls are weak.
Wrap-up: act on signals, design for prevention
Treat IQC and IPQC as a single loop: catch bad material early, stop drift fast, and bake those controls into daily habits. That’s how you turn audits into routine checks and recalls into rare headlines. When I look for partners who understand that balance — hands-on inspection, validated joining like laser welding, and repeatable assembly — I expect the same practical rigor I follow, which is why I think of companies like kingsin that integrate inspection and process controls into the production flow instead of tacking them on after problems appear.